Cavitation in Centrifugal Pumps: Causes, Warning Signs, and Prevention

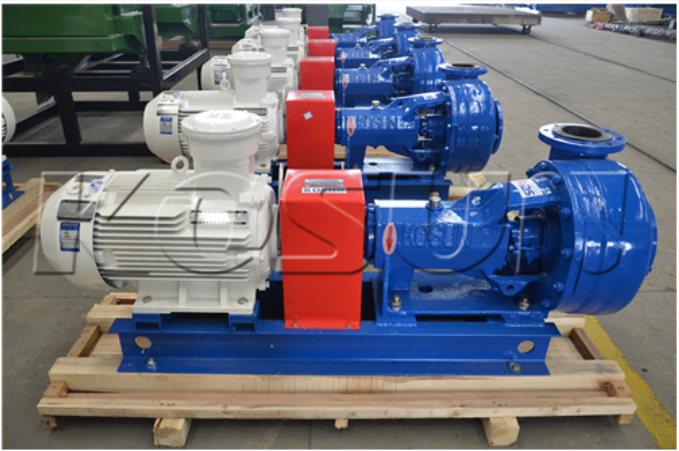
Cavitation ranks among the most destructive conditions a centrifugal pump can face. When local fluid pressure falls below the liquid’s vapor pressure, small vapor bubbles form inside the pump. These bubbles then collapse violently as pressure recovers, sending microscopic shock waves into metal surfaces. Over time, this process erodes impellers, damages casings, and shortens mechanical seal life — outcomes no drilling contractor can afford. Understanding what triggers cavitation and how to stop it is the first step toward protecting your pump investment. KOSUN offers centrifugal pumps engineered for reliable performance in demanding drilling environments.
Understanding Cavitation in Centrifugal Pumps

Before discussing prevention, it helps to know what cavitation looks like in the field. Too often, field teams miss early warning signs, turning a fixable problem into an expensive machine failure.

What Cavitation Looks Like

Cavitation in a centrifugal pump usually produces a rattling or cracking sound — often resembling gravel moving through the case. You may also notice erratic flow rates, fluctuating discharge pressure gauge readings, or visible vibration on the pump body. None of these are normal operating sounds.

How It Progresses

If cavitation pitting on impeller vanes and casing walls goes unaddressed, it worsens. Vibration pushes mechanical seal faces out of alignment, leading to leaks. Bearing loads rise. What begins as noise becomes structural damage that requires replacing the entire pump rather than servicing it.

Why It Matters for Drilling Operations

A centrifugal pump moves slurry between land rigs and offshore platforms, continuously handling rough, heavy fluids. Cavitation compounds the wear these fluids already cause, accelerating degradation far beyond what either problem would produce alone. Even a brief pump outage halts the drilling fluid circuit for mud engineers managing solids control systems.

Root Causes of Cavitation

Cavitation doesn’t appear without warning. It follows predictable patterns tied to fluid conditions, system design, and pump selection. To make the right fix, you need to pinpoint the exact issue in your program.

Insufficient Net Positive Suction Head (NPSH)

The leading cause is usually insufficient available NPSH — when suction-side pressure does not exceed the pump’s required NPSH by a safe margin. This can occur with long suction lines, excessive suction lift, clogged strainers, or high fluid temperatures. Industry standards recommend maintaining at least 3 feet of NPSH above the pump’s rated minimum.

Operating Away from the Best Efficiency Point

Every centrifugal pump has a Best Efficiency Point (BEP) on its performance curve — the flow rate where it operates most efficiently. Running significantly faster or slower than that flow rate alters internal pressure distribution and creates recirculation zones where vapor pockets form. Cavitation becomes a serious risk for pumps forced to operate outside their design conditions for extended periods.

Mechanical and Installation Factors

Worn impellers change internal clearances and reduce hydraulic effectiveness. Air leaks on the suction side, partially closed suction valves, or undersized piping can all restrict flow and lower local pressure. In the field — especially on mobile rigs or frac trucks — vibration can loosen fittings, admitting air and worsening cavitation behavior.

Practical Methods to Prevent Cavitation

Repairing is far more expensive than preventing. Cavitation can be stopped at its source through a structured approach covering system design, operating procedures, and equipment selection.

Optimize the Suction System

Keep suction lines short and straight. Use the largest practical pipe diameter on the suction side. Position the pump as close to the fluid source as possible, and clean suction strainers regularly. These steps raise available NPSH immediately — without modifying the pump itself.

Select the Right Pump for the Application

Off-BEP operation can be avoided when pump volume, head grade, and speed all match system requirements. As long as the centrifugal pump is properly sized for the solids control system’s flow range, it will spend most of its life near its most efficient point, where cavitation risk is lowest. KOSUN centrifugal pumps are built to handle slurry continuously, with open impellers and wide vane profiles that maintain stable fluid flow across a broad operating range.

Implement Routine Monitoring

Regularly checking suction pressure, discharge pressure, and sound levels can catch small problems early. Handheld acoustic monitoring instruments can detect the characteristic cavitation sound at low levels before damage occurs. Maintaining an accurate operating log also helps identify slow performance changes that may signal wear or system drift.

Design and Material Considerations

Hard iron and high chrome metals outperform standard cast iron against the combined attack of abrasive slurry and cavitation-induced pitting. KOSUN centrifugal pumps are available in hard iron , high chrome , aluminum bronze , and stainless steel — giving sourcing teams material options matched to fluid type and wear severity.

An open impeller lowers axial thrust loads, while an impeller retention bolt prevents impeller damage during brief reverse rotation. Wide-vane design improves fluid passage and reduces low-pressure zones where vapor bubbles form. For heavy-duty applications, KOSUN centrifugal pumps feature back vanes on the rotor that prevent solids buildup near the stuffing box and lower internal case pressure, further reducing cavitation likelihood.

Troubleshooting a Suspected Cavitation Event

When noise or performance loss appears, inspect the suction side first — verify valve position, filter condition, and suction line integrity. Then compare the operating point against the pump curve. If the system has changed — flow requirements, longer pipe runs, or different fluid density — adjust NPSH margins before assuming the pump has failed.

Procurement Checklist

When specifying centrifugal pumps, prioritize:

  • Material construction matched to fluid abrasiveness and pH
  • Hydraulic performance curves verifying BEP covers your operating range
  • Seal options and spare seal lead times
  • Spare parts compatibility across pump sizes
  • 24/7 technical support, especially for offshore or remote sites

These requirements lead directly to fewer unexpected shutdowns and lower total cost of ownership.

Conclusion

Cavitation in a centrifugal pump is preventable through correct system design and proper equipment selection. The essentials are suction head margins, operating point accuracy, material durability, and routine monitoring — principles that apply equally on land, offshore, or on mobile rigs. KOSUN manufactures centrifugal pump lines designed for continuous slurry service in demanding oil and gas environments. Choosing a pump built for your specific conditions — backed by responsive technical support and readily available replacement parts — is the most reliable way to keep mud flowing smoothly for the long term.
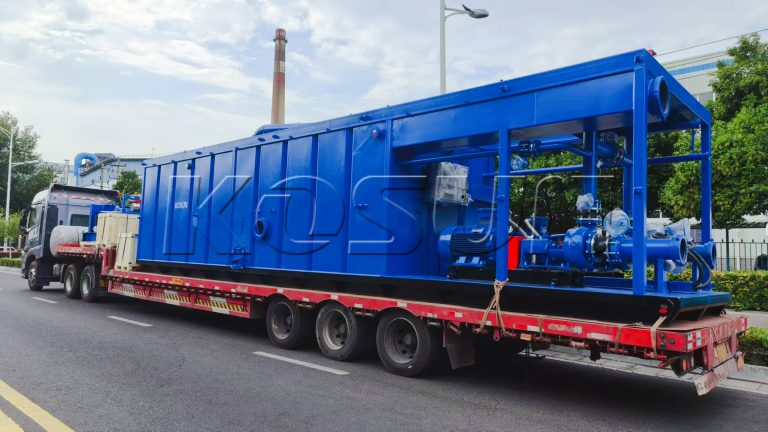
Vacuum Degasser: Protecting Solids Control Assets and Reducing NPT

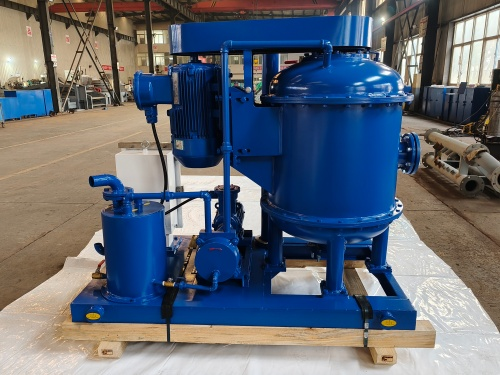
As the global drilling industry pushes for cost reduction and efficiency gains in 2026, minimizing Non-Productive Time (NPT) has become a central objective. Controlling solids content is only part of the equation, eliminating micro-bubbles from drilling fluids is equally critical to protecting expensive solids control assets and trimming maintenance expenditures. Pre-treatment through a vacuum degasser is, in essence, a high-yield investment in asset integrity. KOSUN offers advanced vacuum degassers engineered to protect downstream equipment and extend service life.

Microscopic Cavitation Damage to Precision Metal Surfaces

When gas-cut mud enters centrifugal pumps or high-speed decanter centrifuges, it triggers destructive cavitation. As gas bubbles collapse abruptly in high-pressure zones, the resulting shockwaves repeatedly strike impellers and bearings. Originally smooth metal surfaces become pitted like honeycombs or suffer large-scale spalling, leading directly to the premature scrapping of core components. KOSUN’s vacuum degassers effectively remove entrained gas, preventing cavitation and protecting critical equipment.

Hidden Costs of Volumetric Efficiency Loss and System Energy Consumption

Due to the compressibility of gases, when a mud pump processes gas-entrained fluid, a portion of the power is absorbed by the gas compression process, severely compromising the pump’s volumetric efficiency. This phenomenon also leads to significant pressure fluctuations. Beyond reducing efficiency, the resulting violent vibrations are “silent killers” of high-pressure manifolds and sensors. By degassing, pump pressure fluctuations can be significantly stabilized, protecting consumables such as pistons, valves, and seats, effectively extending their replacement cycles.

Performance Multipliers in Closed-Loop Solids Control Systems

The operational logic of modern solids control systems is interconnected. The presence of gas bubbles artificially inflates the apparent viscosity of the mud, making it thick and difficult to separate. Bubbles act like “glue,” encapsulating fine sand particles and disrupting the stability of the centrifugal field inside hydrocyclones, which compromises the performance of desanders and desilters. As a critical intermediate link, the vacuum degasser ensures that downstream centrifuges achieve precise solid-liquid separation at high speeds by thoroughly eliminating entrained gas.

Strategic Investment Driving OPEX Optimization

The value of a vacuum degasser extends far beyond a single piece of equipment. It creates significant gross margin for drilling contractors by reducing the replacement frequency of expensive spare parts (such as pump fluid end modules and centrifuge drums) and compressing downtime caused by equipment failure. In the capital-intensive world of oilfield services, the vacuum degasser is an essential tool for achieving Equipment Life Cycle Management. KOSUN is committed to providing high-performance vacuum degassers and expert support to help customers achieve their operational and financial goals.

Conclusion

A vacuum degasser is more than just a gas removal device, it is a strategic investment in equipment longevity, operational efficiency, and cost control. By eliminating destructive micro-bubbles, it protects pumps, centrifuges, and downstream equipment from cavitation, wear, and premature failure. For any drilling operation seeking to reduce NPT and optimize OPEX, a high-performance vacuum degasser is an essential component of the solids control system.

Inside the Mud Tank: How It Powers Drilling Fluid Circulation

Every drilling rig depends on a continuous loop of drilling fluid moving from surface to bottom hole and back again. At the center of that loop sits the mud tank, a piece of equipment that often goes unnoticed but quietly makes the entire operation possible. From storing thousands of cubic metres of fluid to separating out damaging solids and stabilising pressure across the system, the mud tank carries responsibilities that directly affect drilling safety and efficiency. KOSUN manufactures high-performance mud tanks built for reliable service in every drilling environment.

What Goes Into a Mud Tank?

A modern mud tank is more than a steel container. It combines a tank body, mixing mechanism, level monitoring system, flow pipelines, and interconnecting fittings into one integrated unit.

The tank body itself is welded from heavy steel plate, engineered to withstand continuous service. Inside, the mixing mechanism keeps solids from settling to the bottom. The level monitoring system tracks fluid height in real time, protecting against overflow on one end and pump starvation on the other. Together, these elements create a system that performs reliably around the clock.

How the Mud Tank Functions

Fluid Storage: The tank holds a stable reserve of drilling fluid, allowing operations to continue without interruption.

Fluid Circulation: Pumps pull mud from the tank and send it downhole; the returning stream carries cuttings back to complete the cycle.

Solids Removal: Vibrating screens, desanders, and desilters installed on the tank strip out cuttings and finer particles, raising mud purity.

Fluid Conditioning: Operators introduce chemical treatment agents to adjust viscosity, density, and other properties according to formation requirements.

Level Management: Sensors monitor mud height and control pump activity to keep levels steady.

Four Critical Roles of the Mud Tank
  1. Storage Capacity That Keeps Drilling Moving

The mud tank’s most fundamental job is holding enough drilling fluid to sustain continuous operations. In ultra-deep wells, that can mean storage capacity measured in thousands of cubic metres.

Beyond routine supply, the tank also acts as an emergency reserve. When a well surge or leak occurs, stored fluid can be deployed immediately to bring downhole conditions under control.

  1. Purification That Protects Equipment

As drilling fluid circulates, it collects rock cuttings. Left in the system, those solids cause equipment damage. Working alongside vibrating screens, desanders, and desilters, the mud tank helps separate solids effectively, extending both fluid performance and equipment service life.

Harmful gases present a second purification challenge. Hydrogen sulphide (H₂S) and methane (CH₄) can dissolve into the fluid, creating safety hazards. Mud tanks address this with gas discharge devices such as breathing valves. More advanced designs incorporate degassers for an added layer of protection.

  1. Blending That Matches Formation Conditions

Drilling fluid properties must be adjusted as formations change. Adding barite increases density, for example, while chemical treatments modify viscosity. Through accurate mixing within the mud tank, operators ensure the fluid meets the demands of each drilling stage.

  1. Stability That Holds the System Together

The mud tank buffers the pressure and flow fluctuations that naturally occur during drilling. When pump output climbs, the tank absorbs the excess fluid; when output drops, it releases stored fluid to fill the gap. This buffering protects equipment and keeps circulation steady.

The tank also serves as the connecting hub between vibrating screens, desanders, desilters, and mud pumps. By linking these components, it maintains orderly flow and keeps every piece of equipment working in harmony.

Conclusion

Mud tanks are far more than storage vessels, they are the backbone of the drilling fluid circulation system. By providing reliable storage, removing solids and harmful gases, enabling precise blending, and stabilising system pressure, they contribute directly to safe and efficient drilling. KOSUN is committed to delivering high-performance mud tanks and expert support to help customers achieve their operational goals.

Drilling Fluid Vibrating Screen: Three Factors That Shape Performance

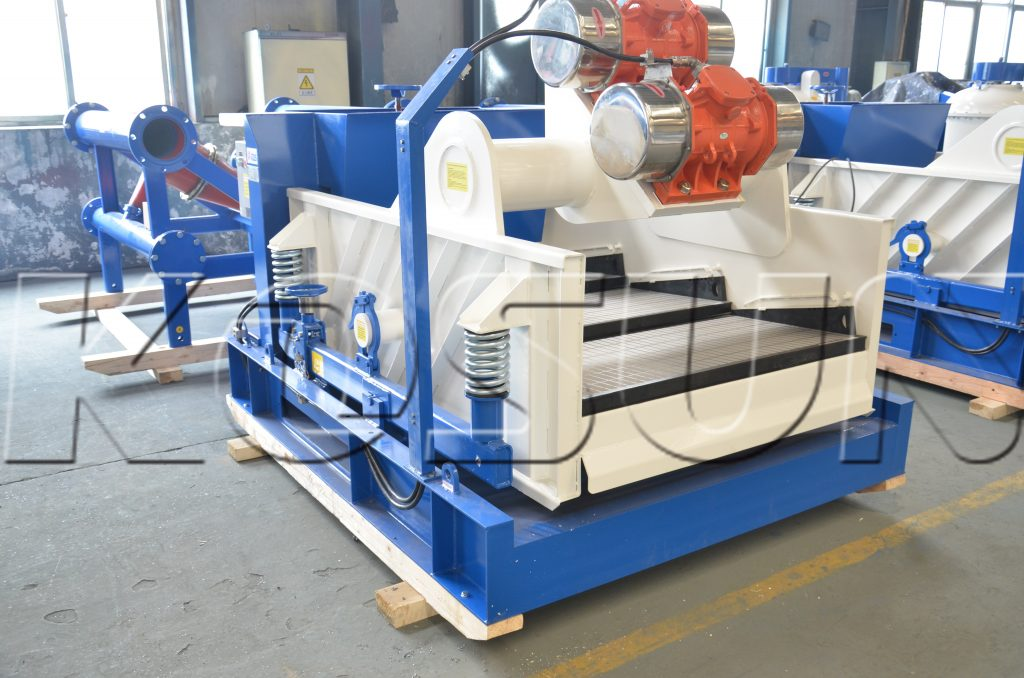
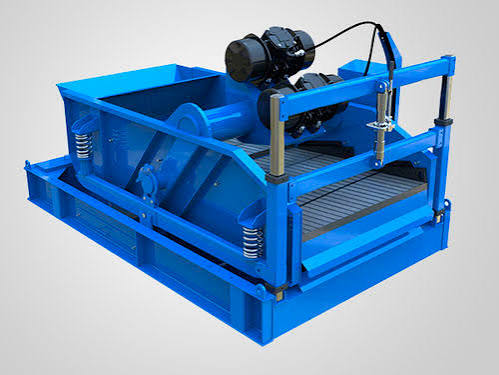
The drilling fluid vibrating screen occupies a unique position in the mud control system. Positioned at the very front of the process, it handles solid-liquid separation earlier, faster, and more economically than any downstream equipment. Its working efficiency effectively sets the processing ceiling for the entire system. Because of this, identifying what drives — or limits — screen performance is essential for any drilling operation. Three factors dominate: vibration mode, amplitude and frequency, and screen mesh characteristics. KOSUN provides high-performance vibrating screens engineered to maximize efficiency across all three dimensions.

Factor One: Vibration Mode

Vibration mode shapes how solids travel across the screen surface. Vibrating screens generally operate in one of three patterns: linear, circular, or elliptical motion. The deciding variable is where the vibrator’s center of gravity sits.

Within the vibrator: The screen produces circular motion.

Above the vibrator: The screen generates elliptical motion, which depends on screen slope to move cuttings — a design that trades processing capacity for conveyance.

Above and slightly forward: The screen delivers linear motion, sustaining a consistent conveying speed.

In practice, linear motion has become the standard for most drilling operations because it balances conveyance and capacity effectively.

Factor Two: Amplitude and Frequency

Amplitude and frequency together control how aggressively the screen processes fluid. Frequency rises and falls with motor speed, and higher frequencies generally improve solid-phase separation. High-frequency vibrating screens, for instance, commonly operate at roughly 2,000 vibrations per minute.

Amplitude describes the vertical travel of the screen, set by vibration mass and eccentricity. Increasing amplitude can strengthen processing performance — but it also raises mechanical stress on the equipment, which can shorten service life. Consequently, operators must weigh separation performance against long-term durability.

Factor Three: Screen Mesh and Material

Screen mesh and material form the final performance layer. Most shale vibrating screens carry 2 to 4 screen layers, with drilling fluid flowing through each in sequence for staged classification.

Choosing the wrong mesh size — or operating with damaged screens — sharply reduces separation efficiency. Faulty installation can also cause premature wear or tearing. For these reasons, correct screen material selection and proper installation are both essential to continuous, reliable operation.

The KOSUN Advantage

KOSUN vibrating screens bring clear strengths to oil drilling applications. Their modular design and high-precision manufacturing ensure smooth, dependable operation. Multiple adjustable vibration modes allow adaptation to different formations and drilling requirements. High-quality motors and shock absorption systems sustain high-frequency screening efficiency while extending equipment life. Finally, high-strength composite screen mesh materials combined with sound structural design significantly boost screen durability and processing efficiency — delivering an economical, all-around solids control solution.

Conclusion

Understanding vibration mode, amplitude and frequency, and screen mesh characteristics gives operators the tools to select and fine-tune their drilling fluid vibrating screen for peak efficiency. The right screen translates into better solids removal, longer equipment life, and reduced drilling costs. KOSUN is committed to providing high-performance vibrating screens and expert support to help customers achieve their operational goals.

Mud Cooling Under Water Scarcity: Solutions for Onshore Drilling

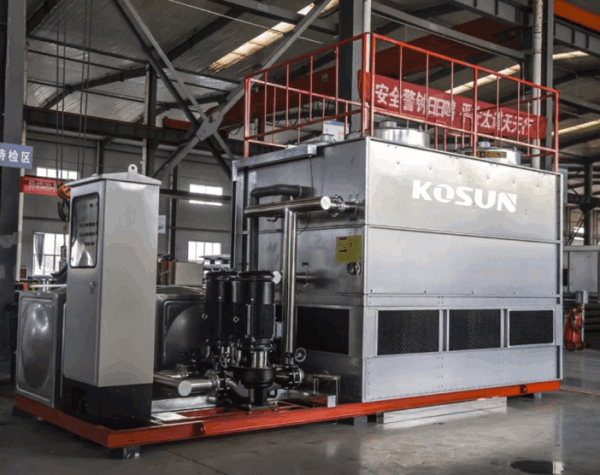
In modern deep-well and geothermal exploration, surface mud cooling represents a critical technical necessity. High bottom-hole temperatures cause circulating fluid to absorb immense thermal energy. Without surface cooling, this cumulative heat triggers severe chemical and mechanical degradation across the drilling asset. Managing this thermal profile is essential for stabilizing fluid chemistry and protecting downhole infrastructure. KOSUN offers advanced mud cooling systems engineered for optimal performance in water-restricted environments.

Onshore Thermal Management: Tailoring Systems to Local Water Access

Onshore equipment selection must align precisely with local utility access and the availability of cooling water. Different water conditions demand different cooling strategies.

  1. Direct Cooling for Water-Abundant Sites

Where water supplies are unrestricted, direct cooling offers an optimized, high-throughput solution. The simple architecture features large-diameter inlet piping to minimize clogging from suspended solids. Operating under standard conditions, systems like the KSNQ-150 utilize a 1.6 MPa design pressure to deliver a stable 20°C to 30°C temperature drop at capacities up to 150 m³/h .

  1. Closed-Circuit Configurations for Water Conservation

When environmental regulations or supply costs demand strict water conservation, a split-system design is required. This setup pairs a large plate heat exchanger with a small cooling tower. This closed-circuit arrangement isolates the active drilling fluid, minimizing evaporation losses while handling displacements up to 200 m³/h .

  1. Air-Cooled Systems for Arid Environments

In desert regions completely devoid of water, operators must rely on ambient air as the heat sink. This setup combines a heavy-duty plate heat exchanger with high-velocity air coolers. It represents a highly sustainable choice for remote fields, offering zero recurring water consumption after the initial equipment investment.

  1. Chiller-Integrated Solutions for Sub-Ambient Cooling

A critical technical bottleneck arises in hot climates when the required target mud temperature falls below the ambient air temperature. In these water-scarce scenarios, a dedicated chiller unit is introduced into the air-cooler circuit. This hybrid process overcomes ambient thermal limits to provide reliable cooling for high-displacement flows up to 200 m³/h .

Offshore Thermal Management: Overcoming Footprint and Corrosion Limits

Offshore platform deployments introduce unique structural constraints. Space margins are extremely tight, and highly corrosive marine environments rule out standard metallurgy.

  1. Titanium Plate Heat Exchangers Utilizing Seawater

Offshore fluid cooling relies on the platform’s most abundant resource: seawater . To withstand aggressive chloride stress corrosion, the system utilizes specialized titanium plate heat exchangers . Titanium provides excellent thermal conductivity alongside absolute resistance to seawater pitting.

Furthermore, this configuration addresses severe deck space limitations by offering a highly compact footprint . These modules can function as standalone units or be linked in parallel combinations to accommodate higher mud displacement volumes during critical-path drilling phases.

Conclusion

Effective thermal management requires a precise engineering match between environmental limits and mechanical architecture. Whether deploying air-cooled desert skids or compact offshore titanium heat exchangers, stabilizing mud temperature remains the primary means of eliminating high-temperature drilling hazards. KOSUN is committed to providing high-performance mud cooling solutions and expert support to help customers achieve their operational goals.

Maximizing Shale Shaker Efficiency in High-Volume Drilling Operations

In high-volume drilling, maximizing shale shaker efficiency is critical for maintaining productivity and controlling costs. Shale shakers are the primary equipment used to separate drill cuttings from drilling fluid. When optimized properly, they improve solids control, reduce waste, and support environmental compliance. This article outlines key strategies, including adjustments to angle and flow rate, preventive maintenance, and modern monitoring systems. KOSUN offers high-performance shale shakers engineered for reliable operation in demanding drilling environments.

Optimal Shaker Angle and Flow Rate Adjustments

Efficient performance depends heavily on shaker angle and flow rate, which directly affect separation quality and fluid recovery.

Fine-Tuning Shaker Angle

Shaker angle strongly influences separation behavior. A steeper angle speeds up fluid drainage, while a shallower angle increases retention time for better solids removal. The right balance depends on:

  • Drilling fluid properties
  • Solids concentration and type
  • Processing capacity requirements
  • Screen mesh size and configuration

Many modern shale shakers allow on-the-fly angle adjustments, enabling operators to respond quickly to changing drilling conditions.

Optimizing Flow Rate

Flow rate must be controlled to avoid screen overload or fluid bypass. Proper optimization considers:

  • Screen capacity and design
  • Fluid viscosity and density
  • Solids loading and particle size
  • Required throughput

Flow control systems and monitoring tools help maintain stable, efficient performance throughout operations.

Preventive Maintenance Strategies

A strong maintenance program is essential for continuous shale shaker operation and reduced downtime.

Maintenance Scheduling
  • Key maintenance practices include:
  • Regular component inspections
  • Timely replacement of worn parts
  • Lubrication of moving systems
  • Screen cleaning and unclogging
Sensor calibration

A proactive approach reduces unexpected failures and keeps performance consistent.

  • Screen Selection and Replacement
  • Shaker screens are central to separation efficiency. Important factors include:
  • Mesh size and screen type
  • Compatibility with drilling fluid
  • Solids load conditions
  • Wear patterns and lifespan

Regular inspection helps identify wear or blinding early. High-quality options like PTS (Pre-Tensioned Screens) can extend service life and improve efficiency.

Advanced Monitoring Systems

Real-time monitoring significantly improves operational control and efficiency.

Sensor-Based Performance Tracking

Modern systems use sensors to track key indicators:

  • Vibration sensors for motion balance
  • Flow sensors for distribution accuracy
  • Pressure sensors for screen loading
  • Temperature sensors for fluid and equipment health
  • These inputs help operators make immediate adjustments.
Predictive Maintenance

Machine learning-based systems can analyze sensor data to:

  • Detect early performance degradation
  • Predict maintenance needs
  • Optimize service schedules
  • Support proactive decision-making
  • This reduces downtime and improves overall equipment reliability.
Conclusion

Maximizing shale shaker efficiency requires optimizing operational settings, maintaining equipment proactively, and using real-time monitoring tools. By adjusting angles and flow rates, implementing structured maintenance, and leveraging predictive systems, operators can improve solids control, reduce downtime, and enhance drilling performance.

As drilling demands increase, adopting advanced shale shaker practices is essential for maintaining efficiency, cost control, and environmental compliance. KOSUN is committed to providing high-performance shale shakers and expert support to help customers achieve their operational goals

Mud Gas Separator: Essential Well Control Equipment for Safe Drilling

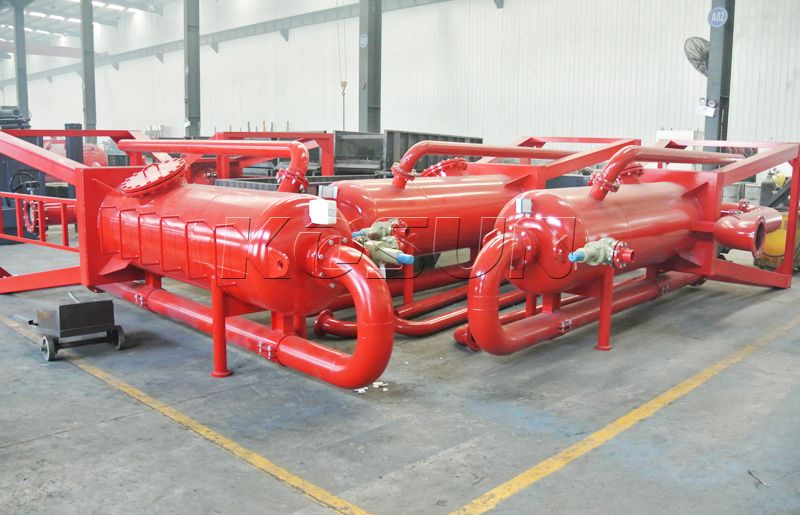
In oil and gas drilling operations, managing gas invasion is a critical safety concern. A mud gas separator — commonly referred to as a poor boy degasser — is a vital component of well control systems, designed to separate and safely discharge gas from drilling fluids. KOSUN provides high-performance mud gas separators engineered for reliable gas handling in the most demanding drilling environments.

Understanding the Mud Gas Separator

A mud gas separator is a specialized vessel used to remove free gas that enters the drilling mud during a kick or when formation pressure exceeds hydrostatic pressure. If left unchecked, gas-contaminated mud loses density and can lead to dangerous well control situations, including blowouts.

The separator operates by directing gas-cut mud through internal baffle plates, which reduce fluid velocity and allow gas bubbles to rise and escape. The liberated gas is then routed through a vent line, typically to a flare system for safe combustion.

Operating Principle of a Mud Gas Separator

When formation gas enters the wellbore, the mud gas separator performs the following functions:

  • Accepts gas-laden drilling fluid from the well
  • Directs flow over internal baffles to slow movement
  • Allows gas to separate from the liquid phase
  • Vents gas to a safe location or flare system
  • Returns cleaned mud to the circulation system

This sequence ensures that well control is maintained and hazardous pressure buildup is avoided.

Where Mud Gas Separators Are Used

Mud gas separators are essential in a variety of drilling scenarios, including:

  • Well control during kicks and pressure surges
  • Blowout prevention systems
  • High-risk formations prone to gas influx
  • Operations involving toxic gases like hydrogen sulfide (H₂S)
  • Situations with incorrect mud weight leading to gas entry

The KOSUN mud gas separator is specifically designed to handle both free and hazardous gases, making it a trusted solution in challenging drilling conditions.

Key Features and Advantages

Modern mud gas separators offer a range of benefits that enhance safety and performance:

  1. High-Efficiency Gas Removal – Effectively extracts large gas volumes from drilling mud, preserving fluid properties and ensuring safe operations.
  2. Controlled Gas Disposal – Gas is directed to a remote flare system, where it is safely burned, reducing risk to personnel and equipment.
  3. Robust and Corrosion-Resistant Construction – Manufactured from high-grade materials with protective coatings to withstand harsh drilling environments.
  4. Improved Well Control – Maintains pressure balance and prevents kicks and blowouts by ensuring gas is removed before mud returns to the wellbore.
Why Mud Gas Separators Are Indispensable

Mud gas separators are a critical part of any well control strategy, offering:

  • Enhanced safety for rig personnel
  • Protection against hazardous gas exposure
  • Reduced environmental impact
  • Improved drilling efficiency
  • Minimized downtime from gas-related problems

Through efficient gas separation and venting, mud gas separators play a key role in maintaining safe and productive drilling operations.

Conclusion

A mud gas separator is more than just a piece of equipment — it is a safeguard against well control incidents and a cornerstone of drilling safety. By effectively removing gas from drilling fluid, it protects people, equipment, and the environment while supporting efficient operations. KOSUN is dedicated to providing reliable mud gas separators and expert support to help customers maintain the highest standards of safety and performance.


Mud Tank: Essential Component for Efficient Drilling Operations

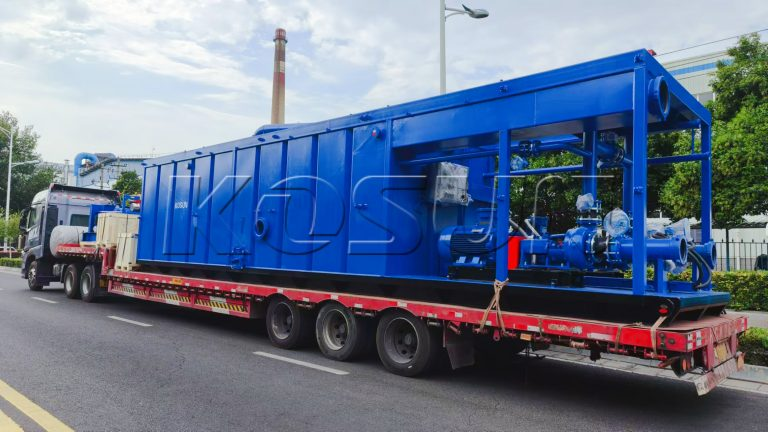
In the field of drilling operations, efficiency, accuracy, and safety are of utmost importance. The mud tank is one of the key components to ensure the smooth operation of the drilling platform. In this paper, we discuss the significance, function, and characteristics of oil rig mud tanks and reveal the importance of mud tanks for drilling rigs in the oil and gas industry. KOSUN offers high-performance mud tanks engineered for reliable drilling fluid management in demanding environments.

Understanding the Mud Tank System

Mud tanks are specialized containers for the storage and circulation of drilling fluids (also known as drilling mud) during drilling operations. These tanks are designed to withstand the rigors of the drilling site and facilitate the management of drilling fluids throughout the drilling process.

The drilling mud tank is the main storage container for drilling fluids, which can hold the large amount of mud required for drilling operations. It also helps in the mixing and blending of drilling fluids to ensure the uniformity and consistency of mud composition. Mud tanks contain mechanisms for separating solids, such as linear motion shale shakers and decanter centrifuges , to maintain the quality and performance of drilling mud. In addition, some advanced mud tank systems include heating and cooling elements to regulate the temperature of the drilling fluid, optimize its performance, and improve drilling efficiency.

Internal Structure of a Drilling Mud Tank

A drilling mud tank is composed of a tank body, mixing device, discharge port, and feed port.

  1. Tank Body

The body of the mud tank is a sealed container, usually made of welded steel plates. The tank has different shapes such as round, oval, or square, and the size also varies according to the specific use needs. The inner wall of the tank is generally treated with anti-corrosion to prevent the corrosion of the mud on the tank.

  1. Mixing Device

A mixing device is provided inside the mud tank for mixing mud to keep it in a uniform mixing state. The stirring device is usually composed of a motor, a reducer, and a stirrer. The motor transmits power through the reducer to the agitator, which rotates the mud to keep the solids suspended and prevent them from settling at the bottom of the tank.

  1. Discharge and Feed Ports

The mud tank is provided with a discharge port and a feed port for the discharge and entry of mud. The discharge port is usually located at the bottom of the tank and drains the mud through a pipe to the next treatment unit. The feed port is usually located at the top of the tank, and the fresh mud is injected into the tank through the pipe. The location and size of the discharge and feed ports are determined according to the specific design requirements in order to achieve effective mud flow and handling.

We usually add a sand pump beside the tank to provide power to transport mud, and sometimes we have a jet mud mixer to mix the mud.

Conclusion

In the dynamic world of drilling operations, mud tanks are an indispensable asset, providing the necessary infrastructure to effectively manage drilling fluids. From storage and mixing to separation and temperature control, drilling rig mud tanks play a multifaceted role in ensuring the success and safety of drilling operations. With the development of drilling technology, the importance of well-designed and reliable solids control equipment has increased, and it is the backbone of the oil and gas industry as it seeks energy exploration and production. KOSUN is committed to providing high-performance mud tanks and expert support to help customers achieve their operational goals.

Cuttings Dryer: Working Principle and Core Functions for Drilling Waste Management

In modern petroleum drilling engineering, as environmental regulations become increasingly stringent, the effective treatment of oily drill cuttings has become a focal point of the industry. As the core equipment of the Drilling Waste Management System, the cuttings dryer has become the key to achieving mud recovery and waste reduction through its superior solid-liquid separation performance. KOSUN offers advanced cuttings dryers engineered for high-efficiency solids control in demanding drilling environments.

Definition and Application Scenarios of the Cuttings Dryer

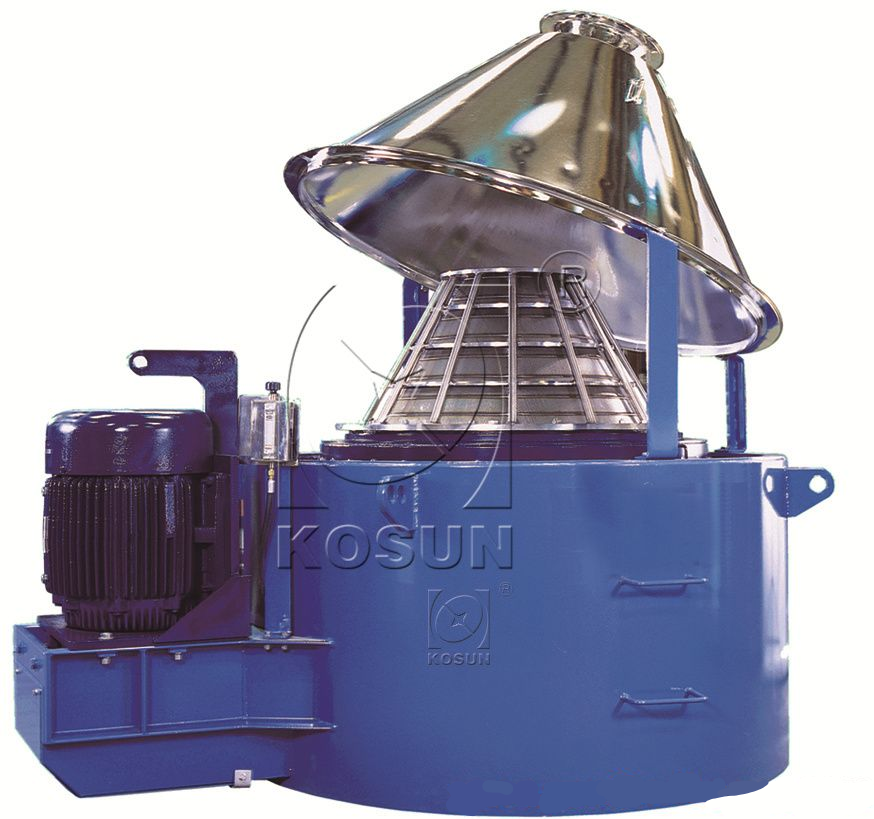
A cuttings dryer (also commonly referred to as a vertical dryer or drill cuttings dryer) is primarily used to treat cuttings generated during drilling processes using Oil-Based Mud (OBM) or Synthetic-Based Mud (SBM). Its core objective is to strip and recover the liquid adhering to the surface of the cuttings using the immense centrifugal force generated by high-speed rotation. This process achieves solid-liquid separation, resulting in drier solids and a significantly reduced oil content on the waste. KOSUN’s cuttings dryers are designed for maximum fluid recovery and minimal waste volume.

Detailed Working Principle of the Cuttings Dryer

Feeding and Acceleration Phase

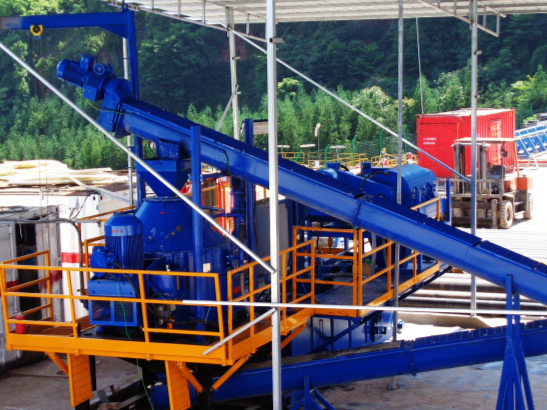
Oily drill cuttings are fed into the top inlet of the cuttings dryer via conveying equipment (such as a Screw Conveyor ). Upon entering the equipment, the cuttings drop into the center of the high-speed rotating basket (screen).

High G-Force Centrifugal Separation Phase

The rotor (containing the screen basket) rotates at high speeds, generating a centrifugal force (G-force) typically ranging from 300G to 900G . Under this intense force, the oil-based liquid adhering to the solid surfaces passes through the screen gaps and enters the liquid collection tank, while solid particles larger than the screen gaps are retained on the inner side of the screen.

Mechanical Scraping and Assisted Discharge Phase

To prevent solids from accumulating and clogging the inner walls of the screen, the cuttings dryer is designed with internal rotating flights (scrapers). There is a slight speed differential between the scrapers and the screen basket. This controlled differential operation scrapes the dried solids off the screen, allowing them to move toward the discharge outlet at the bottom of the equipment under the influence of gravity.

Liquid Recovery and Purification Phase

The expelled liquid phase (mud containing a small amount of fine particles) is discharged through the liquid outlet. Typically, this recovered liquid is sent to a downstream Decanter Centrifuge for further purification. Once ultra-fine particles are removed, the liquid is finally reintroduced into the active mud system for reuse.

Key Technical Parameters Affecting Cuttings Dryer Efficiency

To achieve optimal treatment results under the latest environmental standards, the following parameters are critical:

  • Screen Gap: Typically selected based on the geological formation and lithology.
  • Centrifugal Force: Higher rotational speeds yield greater centrifugal force and better dehydration; however, this places higher demands on the equipment’s dynamic balance and wear resistance.
  • Scraper Wear Resistance: Since drill cuttings are highly abrasive, high-performance cuttings dryer scrapers are usually reinforced with tungsten carbide or other hard alloys to extend their service life.

KOSUN’s cuttings dryers are engineered with durable materials and precision components for long-term reliability in abrasive drilling environments.

Conclusion

Through efficient physical separation, the cuttings dryer not only solves environmental discharge challenges in oilfield operations but also saves drilling contractors significant material costs through high-ratio mud recovery. KOSUN is committed to providing high-performance cuttings dryers and expert support to help customers achieve their operational and environmental goals.

Drilling Fluid Centrifuge: How to Choose the Right One for Your Operation

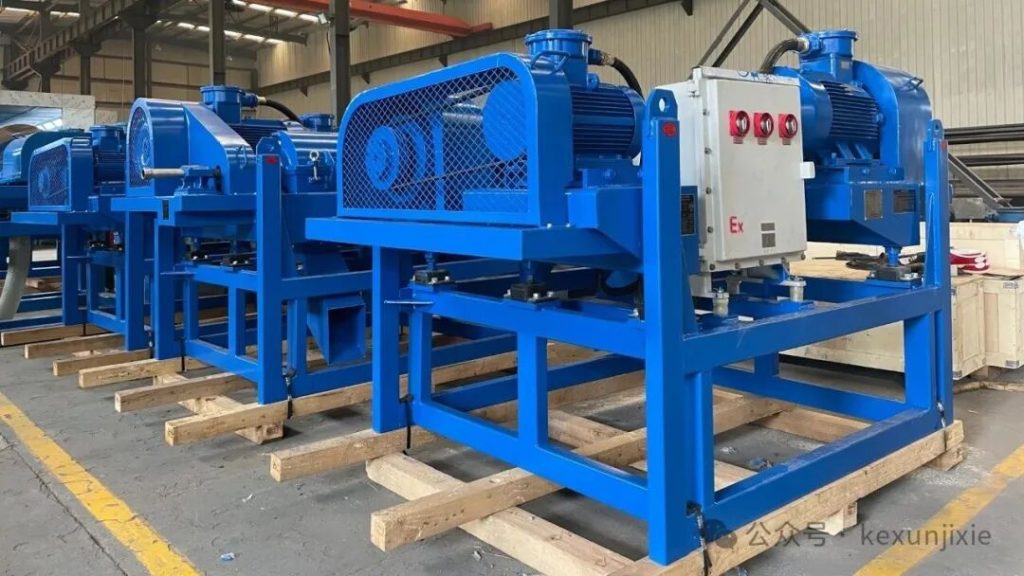
In oil drilling engineering, drilling fluid centrifuges have become indispensable. Their primary job is straightforward but critical: separate solid particles from the drilling fluid to maintain its performance and quality. Choose the wrong drilling fluid centrifuge, and you risk poor solids control, increased mud costs, and unnecessary wear on downstream equipment. Choose the right one, and you improve drilling efficiency, reduce operating expenses, and minimize environmental impact. So how does an operator make the right choice? KOSUN offers a comprehensive range of drilling fluid centrifuges engineered for high-performance solids control in demanding oilfield applications.

Understanding the Basic Types of Drilling Fluid Centrifuges

The first step is to understand the basic types of drilling fluid centrifuges. Generally, they fall into three categories:

  • The sedimentation centrifuge uses centrifugal force to cause solid particles to settle in a high-speed rotating drum — it is the workhorse of most oilfield solids control systems.
  • The separation centrifuge uses high-speed rotation to separate liquids and solid particles of different densities.
  • The filter centrifuge relies on a filter medium to separate solids from liquids.

For most oil drilling applications, the sedimentation centrifuge is the standard choice, particularly for barite recovery and fine solids removal. KOSUN’s sedimentation centrifuges are designed for maximum efficiency and reliability.

Considering the Drilling Fluid Properties

Once you understand the types, consider the drilling fluid itself. Density is first: high-density drilling fluids require higher centrifugal force to separate solid particles effectively. A drilling fluid centrifuge that works well on light mud may struggle with weighted systems. Viscosity is next: high-viscosity fluids require stronger drilling fluid centrifuges to prevent clogging. Solid content also matters: fluids with high solid content need more efficient separation equipment. The heavier the solids loading, the more robust the drilling fluid centrifuge must be.

Evaluating Processing Capacity

After matching type to fluid properties, evaluate processing capacity. This includes throughput volume — how much fluid the drilling fluid centrifuge can process per hour — and separation efficiency — the proportion of solids it actually removes. There is often a trade-off: higher throughput may mean lower efficiency, and vice versa. Generally, the higher the processing capacity you demand, the larger the size and power requirements of the drilling fluid centrifuge will be. Operators must honestly assess rig space and available power.

Additional Selection Factors

Beyond type, fluid properties, and capacity, several additional factors matter:

  • Bowl speed (G-force) determines how fine a cut the centrifuge can achieve — higher speeds remove finer solids but increase wear.
  • Differential speed between bowl and conveyor affects solids discharge rate.
  • Material construction is critical: drilling fluids are abrasive, so drilling fluid centrifuges with wear-resistant components like tungsten carbide tiles last significantly longer.
  • Maintenance requirements should never be an afterthought — a difficult-to-service centrifuge leads to costly downtime.
  • Automation features like variable frequency drives help operators optimize performance as downhole conditions change.

KOSUN centrifuges are built with durable materials, advanced automation, and easy-maintenance designs for long-term reliability.

Conclusion

Choosing the right drilling fluid centrifuge requires understanding the three basic types, matching them to your fluid’s density, viscosity, and solid content, and balancing throughput against separation efficiency. Bowl speed, wear-resistant materials, maintenance access, and automation features all play important roles. A well-chosen drilling fluid centrifuge recovers valuable barite, removes fine solids, reduces waste disposal costs, and extends equipment life. For any serious oil drilling operation, taking the time to select the right drilling fluid centrifuge is time very well spent. KOSUN is committed to providing high-performance centrifuges and expert guidance to help customers make the right choice.